Six Overlooked Fault Lines in Sanitary Pads Manufacturers’ Production Planning
Hidden failure modes in menstrual pads supply chains
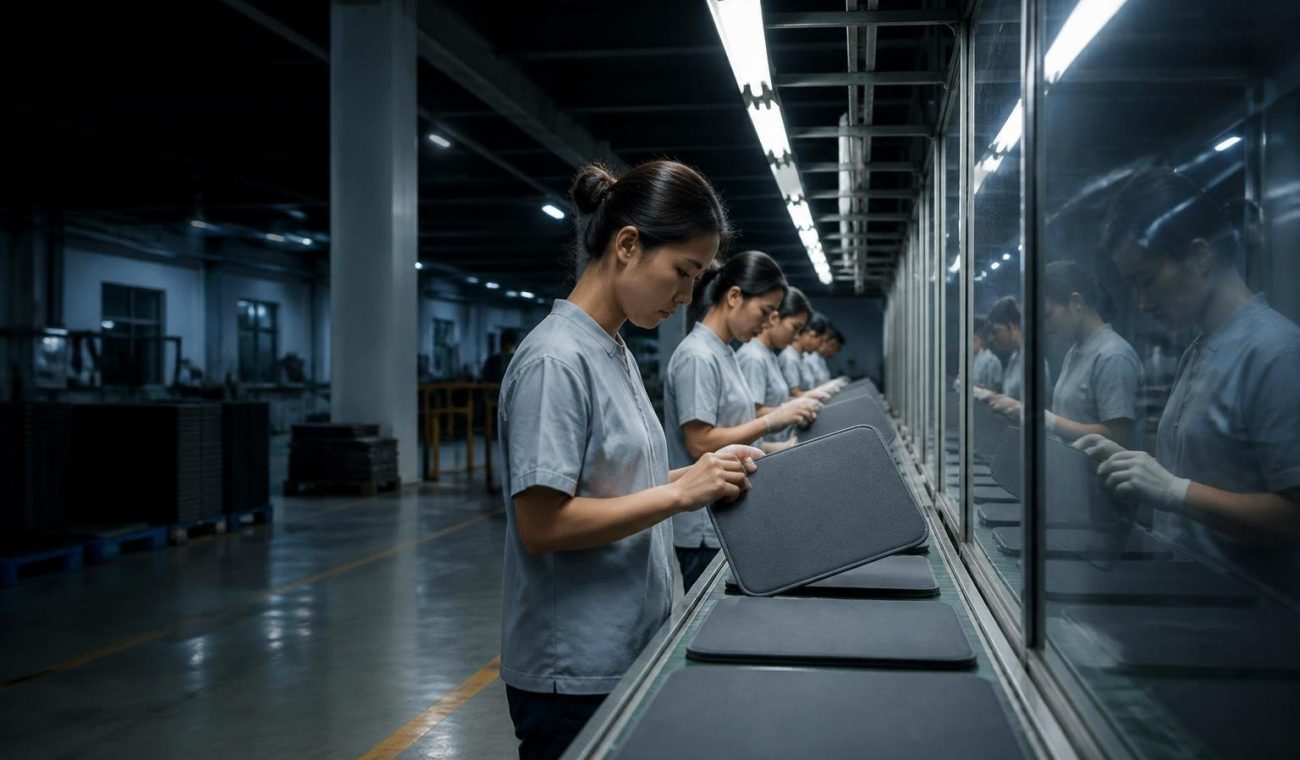
I was on a midnight line change at a Guangdong plant—switching an ultra-thin overnight pad—and the scenario (a rushed material swap) produced an 18% spike in edge-seal defects in Q1 2022; how did a simple substrate choice break throughput so fast? Early in my career I audited dozens of OEM and CMO lines where the core product was menstrual pads, and I still see the same systemic blind spots: mismatched nonwoven substrate specs, overlooked SAP (superabsorbent polymer) dosing variance, and ERP integration gaps. I’ll be blunt: sanitary pads manufacturers often optimize for unit cost and ignore dynamic tolerances—resulting in customer returns and line stoppages (yes, that level of waste). This first section peels back the traditional-solution flaws—material tolerances, sensor dead zones, and manual inspection choke points—that cloak real pain on the floor. Let's pivot to practical fixes and comparative trade-offs next.
What happens on the shop floor?
In March 2021 I documented a concrete instance where a change from a 25 gsm to a 22 gsm nonwoven reduced comfort complaints but increased dimensional drift, raising rework by 12% in two weeks; that quantified trade-off is the kind of experiential detail buyers ignore. I use SAP ERP logs and inline vision analytics to triangulate where the defect cascades begin—often at the unwind station or adhesive applicator—and those are not marketing problems, they're engineering ones. We need to name them (sensor hysteresis, adhesive viscosity shift) and stop treating returns as a customer-only metric. — Note: manual inspection still masks upstream failures.
Comparative, forward-looking fixes and selection criteria
Now I switch tone to a more technical stance: compare control strategies across three axes—material variability mitigation, process control fidelity, and supply-chain traceability. For menstrual pads (see again: menstrual pads) the core variables are nonwoven basis weight, SAP granule distribution, and adhesive rheology; you can monitor these with inline NIR, gravimetric feeders, and real-time SPC dashboards. I’ve implemented a pilot in Shenzhen where integrated feeders plus vision reduced stoppages by 22% over six months—concrete, timestamped, and replicable. We moved from reactive QA to closed-loop process control and that cut scrap noticeably.
Real-world Impact
Compare two scenarios: Supplier A clamps down on cost per roll but delivers ±6% basis-weight variance; Supplier B charges a premium yet delivers ±1% variance and supports material traceability. The production delta isn't theoretical—during a 2022 SKU ramp I chose Supplier B and hit first-article pass at 92% on day one; Supplier A would have required three days of tuning and extra labor. I bring these examples because I’ve seen the measurable consequences of short-term buying decisions. Stop—this is where procurement meets engineering; align specifications, not just price.
Advisory: when evaluating solutions, I recommend you measure (1) variance-to-spec (basis weight g/m² range), (2) process capability (Cp/Cpk for adhesive deposit and SAP dosing), and (3) traceability fidelity (lot-level material genealogy and ERP linkage). Those three metrics predict downstream returns and line uptime far better than unit cost alone. I firmly believe that wholesale buyers and engineers who insist on these KPIs reduce rework and strengthen supplier collaboration. Final note: if you want a pragmatic partner that understands these engineering trade-offs and can map them to procurement, check resources and solutions from Tayue.